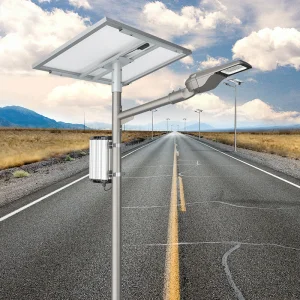
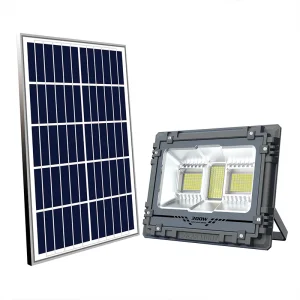
Explore our premium product series featuring high-efficiency architectures, extreme ingress protection, and state-of-the-art power design.
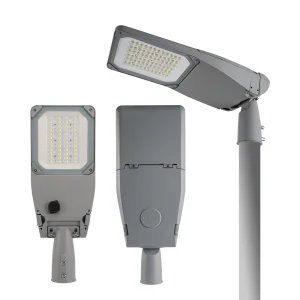
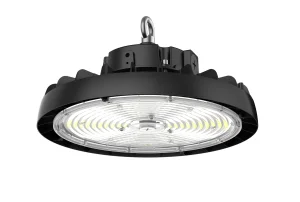
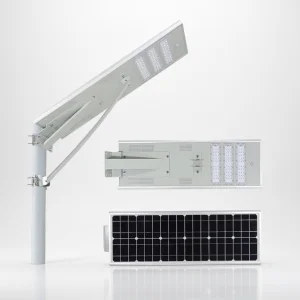
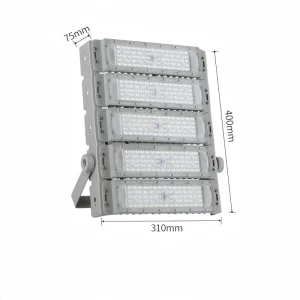
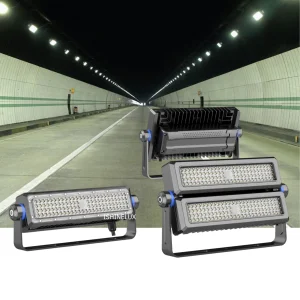
Modern industrial complexes, mega warehouses, distribution hubs, and high-ceiling manufacturing spaces demand more than simple illumination. As corporate entities aim for deep decarbonization and strict operational cost containment, lighting infrastructure has transitioned into a highly technical asset. The global commercial sector is moving rapidly towards high-efficacy solid-state lighting arrays engineered to deliver massive lumen payloads while maintaining high reliability in tough ambient conditions.
Key Market Driver: Energy optimization protocols require high bay lighting configurations to deliver exceeding 160-170 lm/W luminous efficiency, ensuring massive electrical expense reductions.
Converting traditional 400W metal halide (HID) fixtures to high-efficiency 150W LED high bays achieves direct energy reduction values of over 60%. Combined with automated motion sensors and daylight harvesting controllers, overall savings frequently exceed 75% per hub facility.
Large-scale production plants run 24/7/365. High bay setups must feature dynamic thermal dissipation profiles, heavy dust and moisture protection barriers (IP65, IP66, IP67), and explosion-proof chassis to protect workers and maintain unbroken operations.
Narrow corridors, high aisles, and wide assembly lines require custom optic profiles. Utilizing precise 60°, 90°, or 120° beam distribution patterns prevents light leakage, maximizes foot-candle levels on workplanes, and minimizes worker fatigue.
Years Industrial Experience
Highest Optical Efficiency
Engineered Operational Lifetime
ISO & CE Certified Production
Industrial environments expose optical equipment to extreme temperatures, heavy vibrations, voltage fluctuations, and chemically challenging air conditions. We design our industrial fixtures with integrated safety, utilizing pure ADC12 die-cast aluminum heat sinks, isolated premium LED drivers (MeanWell / Sosen), and high-grade optical polycarbonate lenses.
Procurement teams need to carefully evaluate key electrical and optical metrics. The table below details what engineers look for in high bay light specifications compared to cheap alternatives.
| Key Parameter | Standard Industrial Grade | Premium Engineered Grade | Procurement ROI Impact |
|---|---|---|---|
| Luminous Efficacy | 130 - 140 lm/W | 160 - 170 lm/W | Lowers energy draw by up to 20% for the same light output. |
| CCT & Wattage Control | Fixed Power/Color Temp | Switchable (3000K-5000K) | Reduces stockkeeping unit (SKU) counts; adapts to varying installation heights. |
| Junction Temp Management | Tj < 85°C at 25°C ambient | Tj < 70°C at extreme temps | Slows down LED degradation, maintaining brightness over 60,000+ hours. |
| Surge Protection (SPD) | 4kV to 6kV | 10kV / 20kV Industrial Grade | Prevents driver failure caused by grid instability and lightning strikes. |
Yangzhou OneAll Lights Co., Ltd. is a professional manufacturer and exporter specializing in outdoor and industrial lighting solutions. Established in 2003 and located in Yangzhou, Jiangsu Province, China, we have over 20 years of experience in the design, development, manufacturing, and supply of high-quality lighting products for customers around the world.
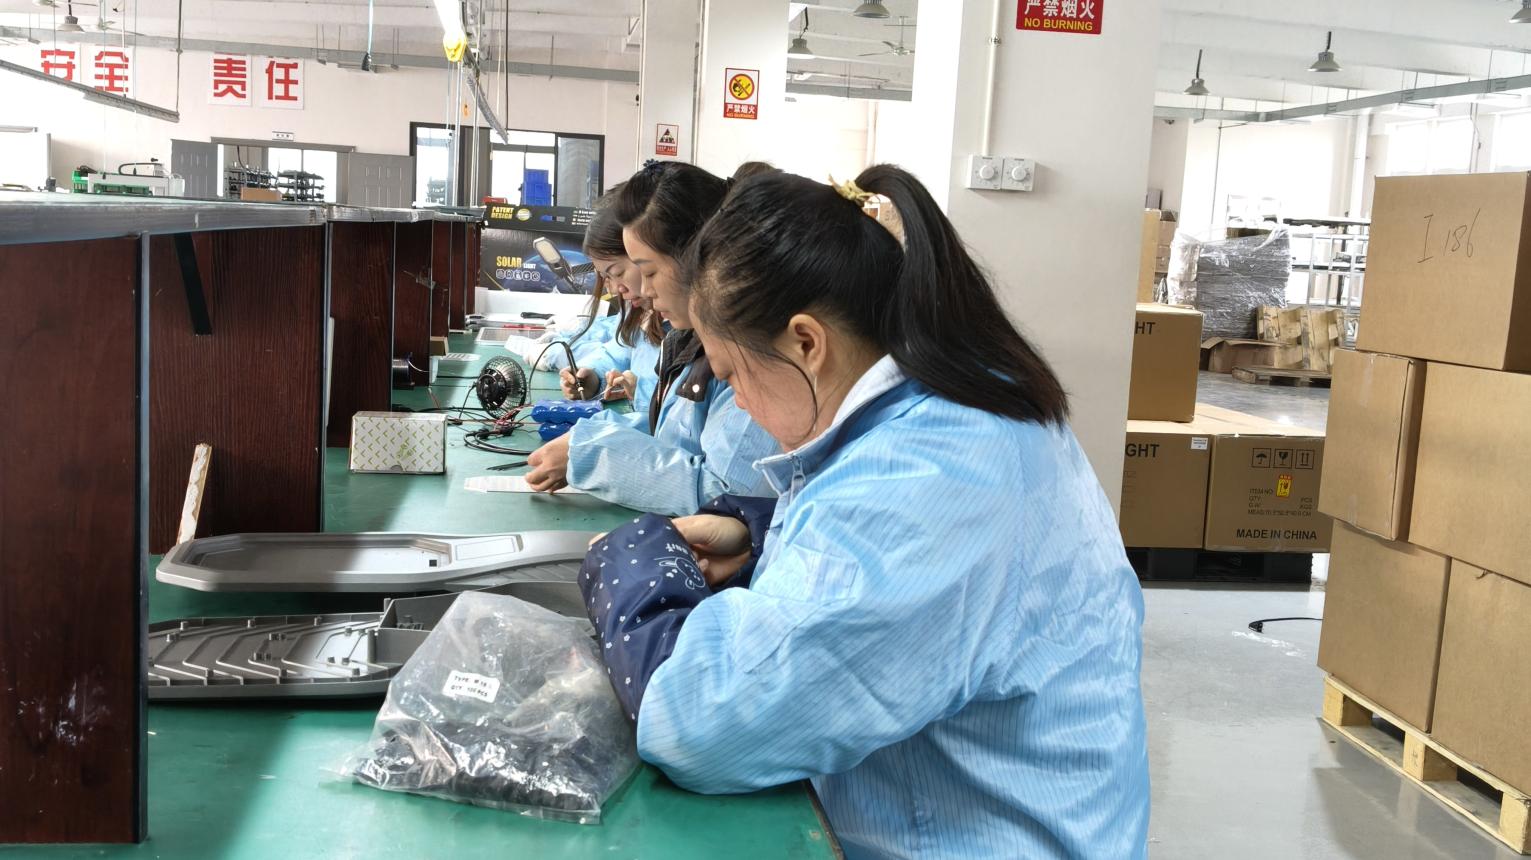
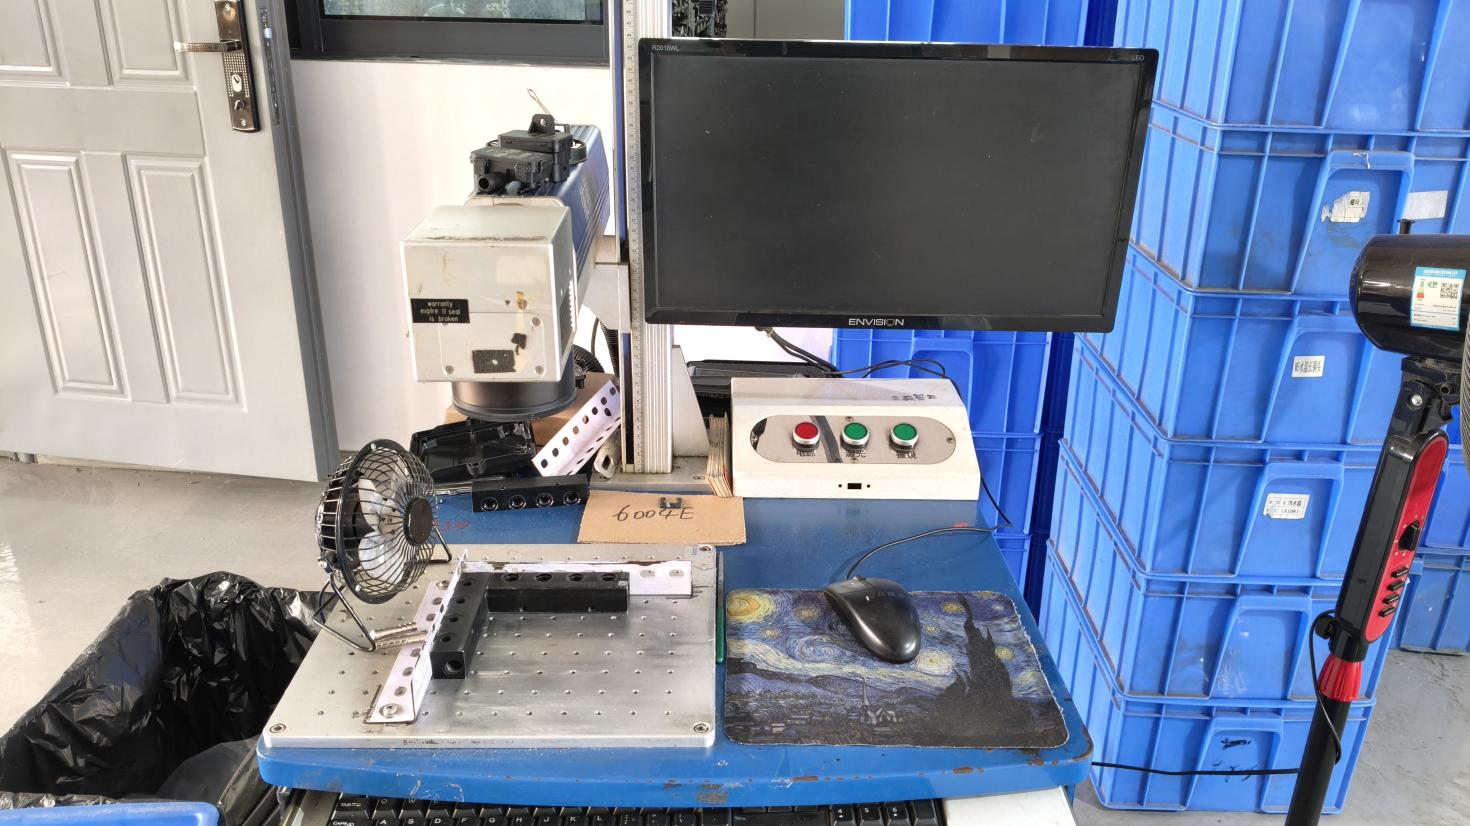
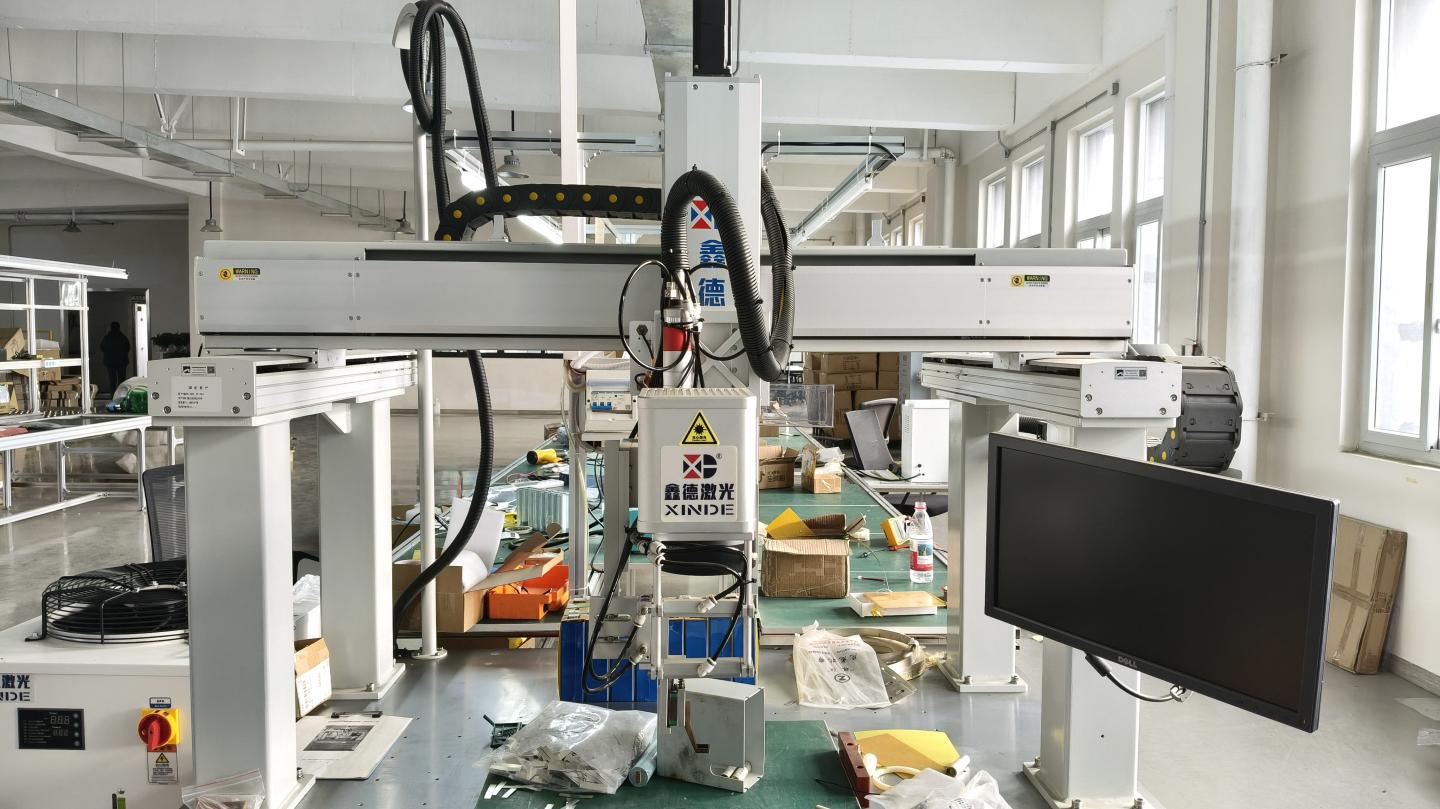
With continuous investment in advanced manufacturing technology, our factory is equipped with modern production facilities, including CNC bending machines, automatic submerged arc welding systems, laser cutting equipment, electrostatic powder coating lines, fluorocarbon painting workshops, and precision testing instruments. Supported by multiple automated production lines and a skilled technical team, we are able to provide efficient production, stable quality, and reliable delivery for projects of all sizes.
Innovation and quality are the driving forces behind our growth. We have established an experienced R&D team dedicated to developing energy-efficient, environmentally friendly, and intelligent lighting solutions that meet the evolving needs of global markets. From product design and engineering to manufacturing and quality inspection, every production process is carried out under strict quality control standards to ensure excellent performance, durability, and long service life. Our company has obtained ISO9001 Quality Management System Certification, ISO14001 Environmental Management System Certification, CCC, CQC, CE certification, and various product testing reports, demonstrating our commitment to international quality and safety standards.
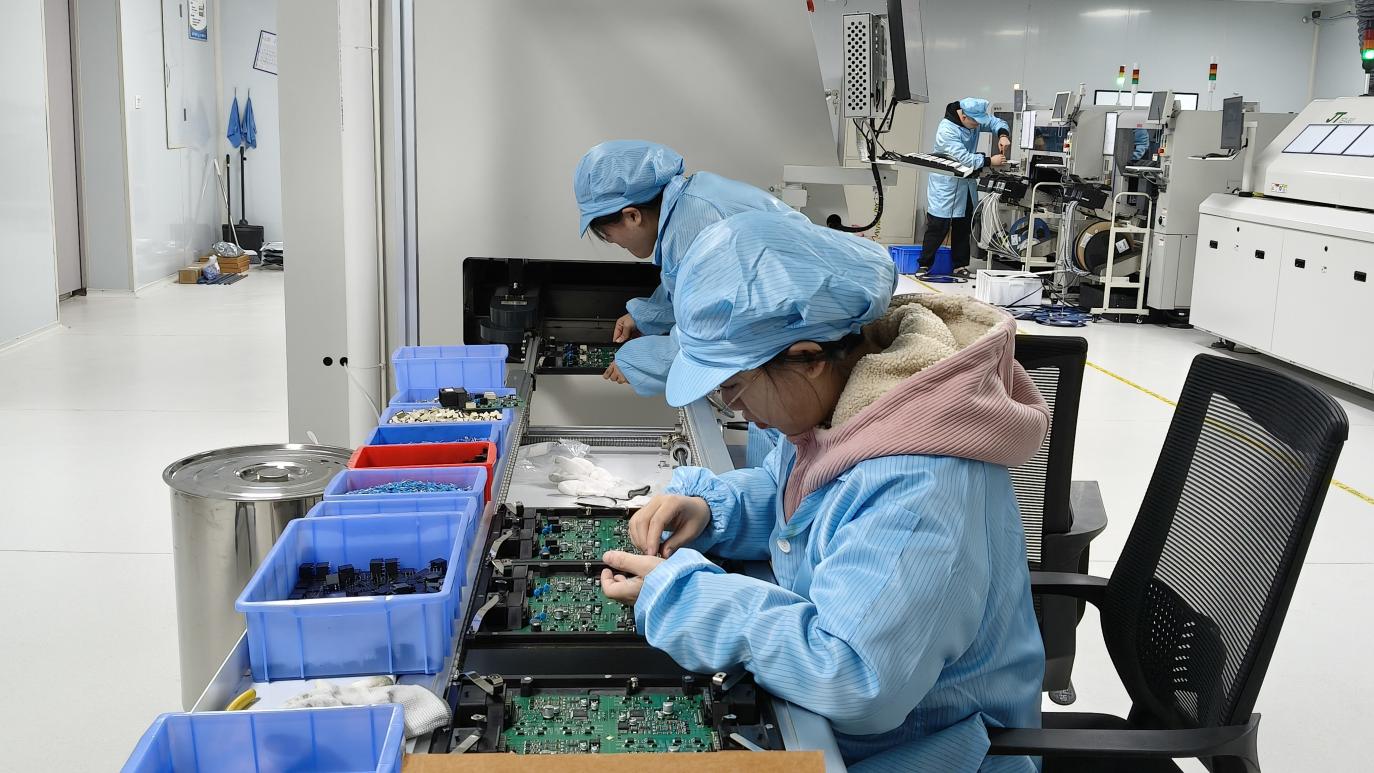
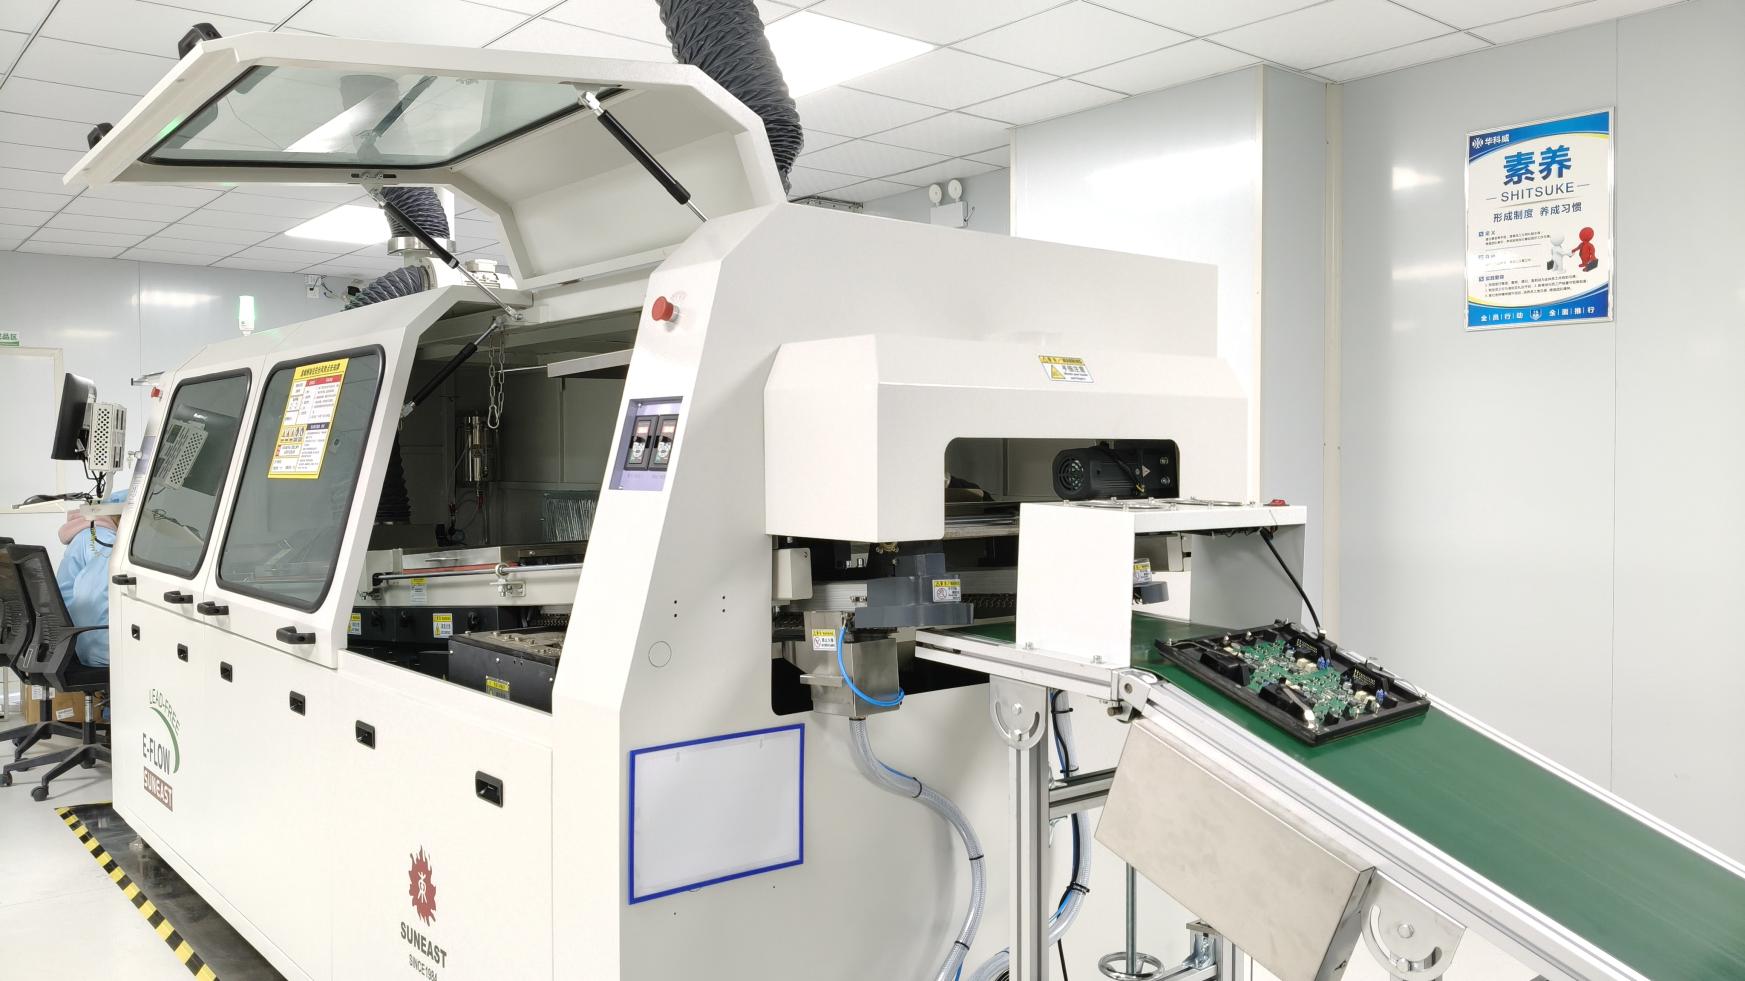
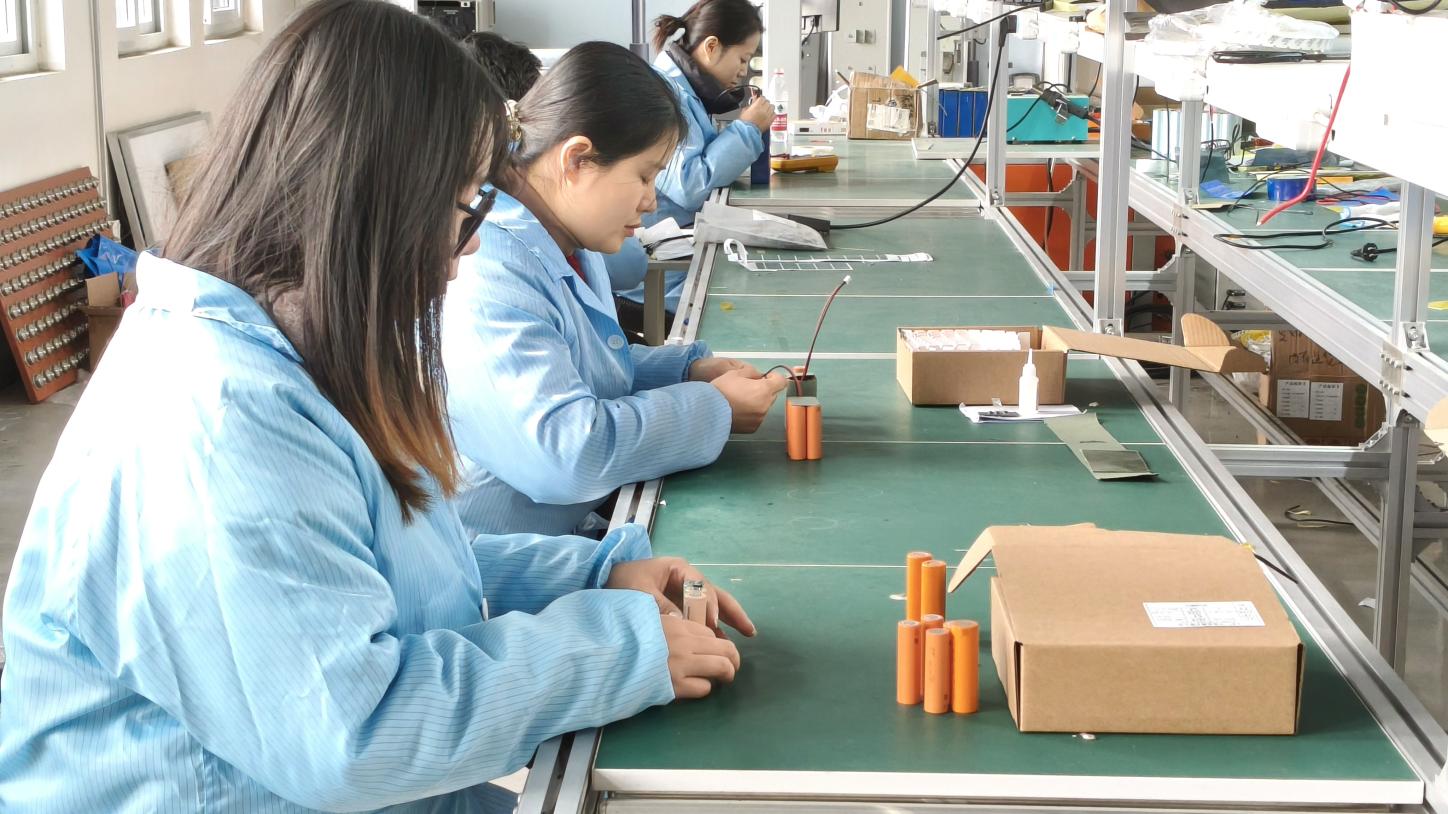
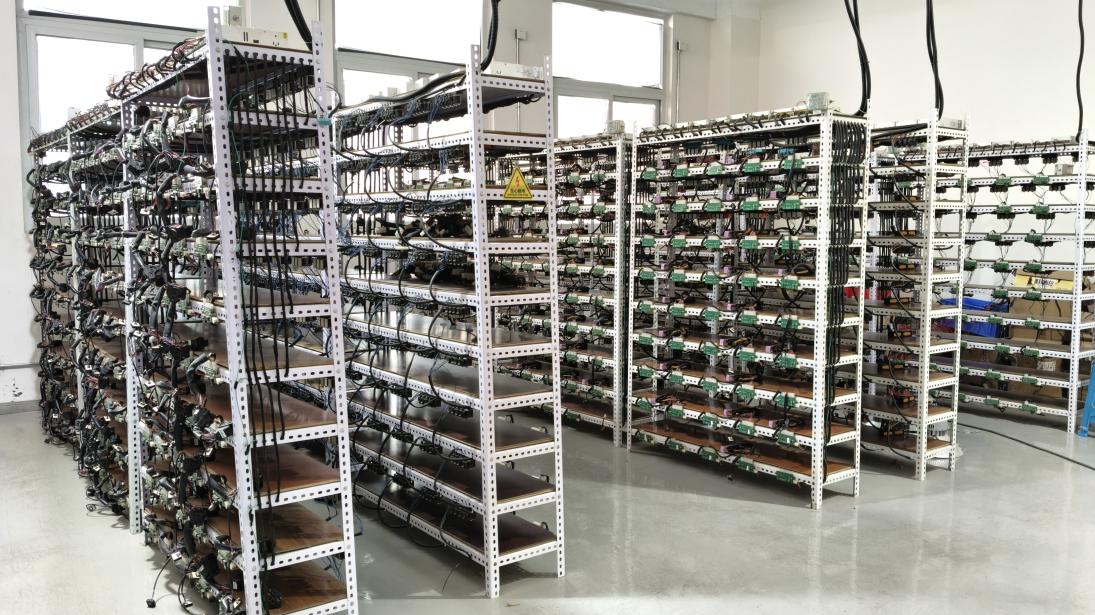
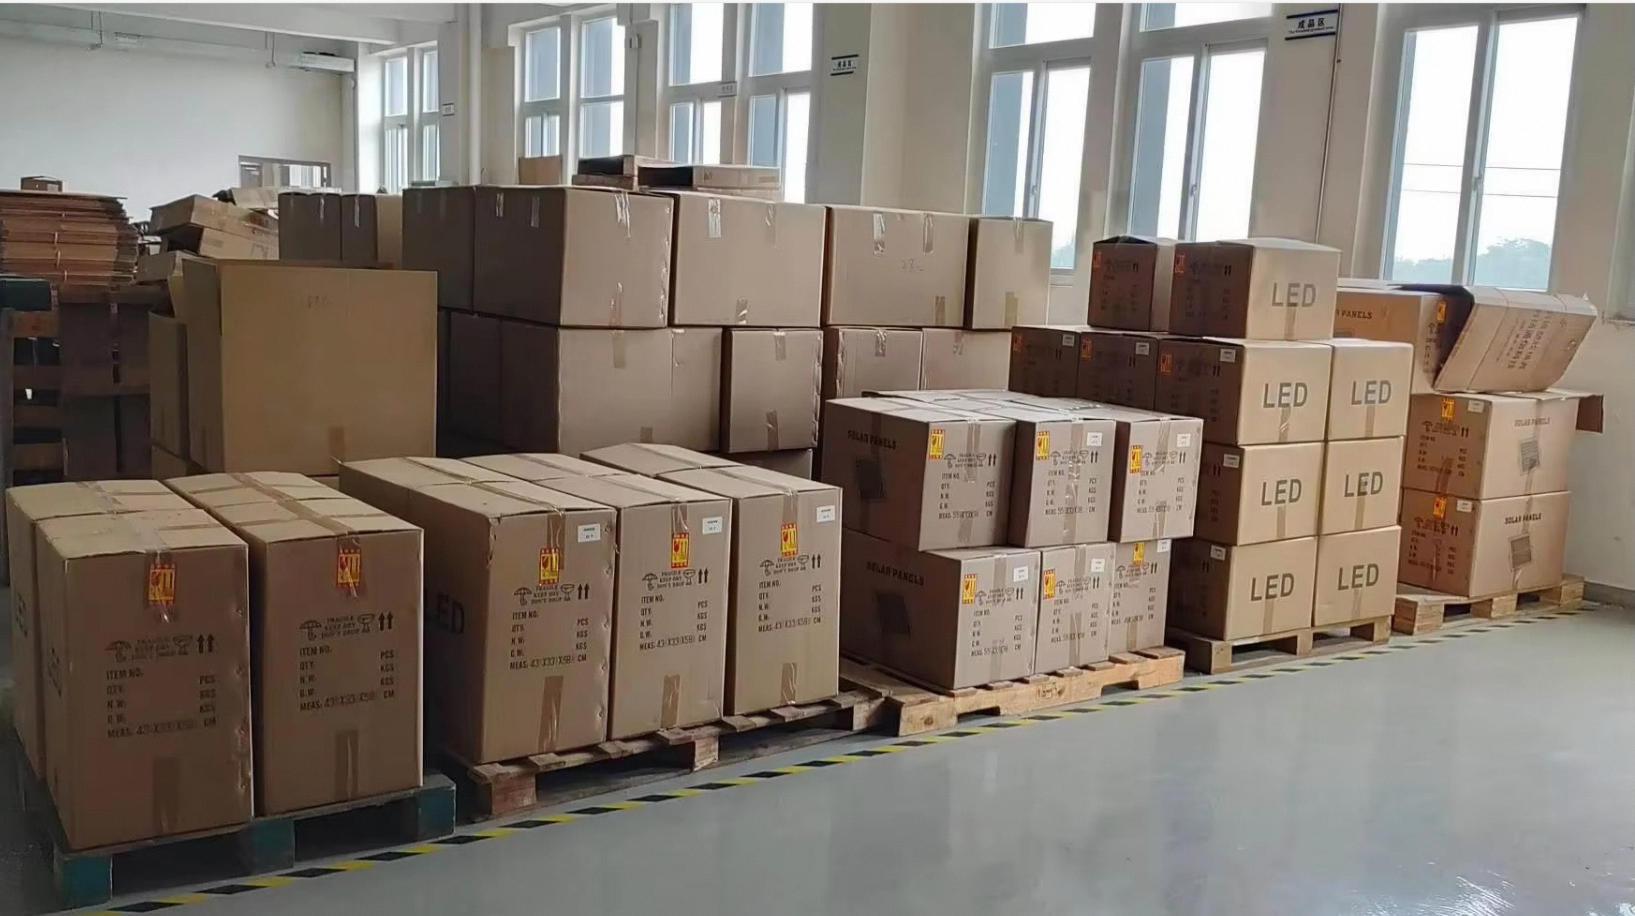
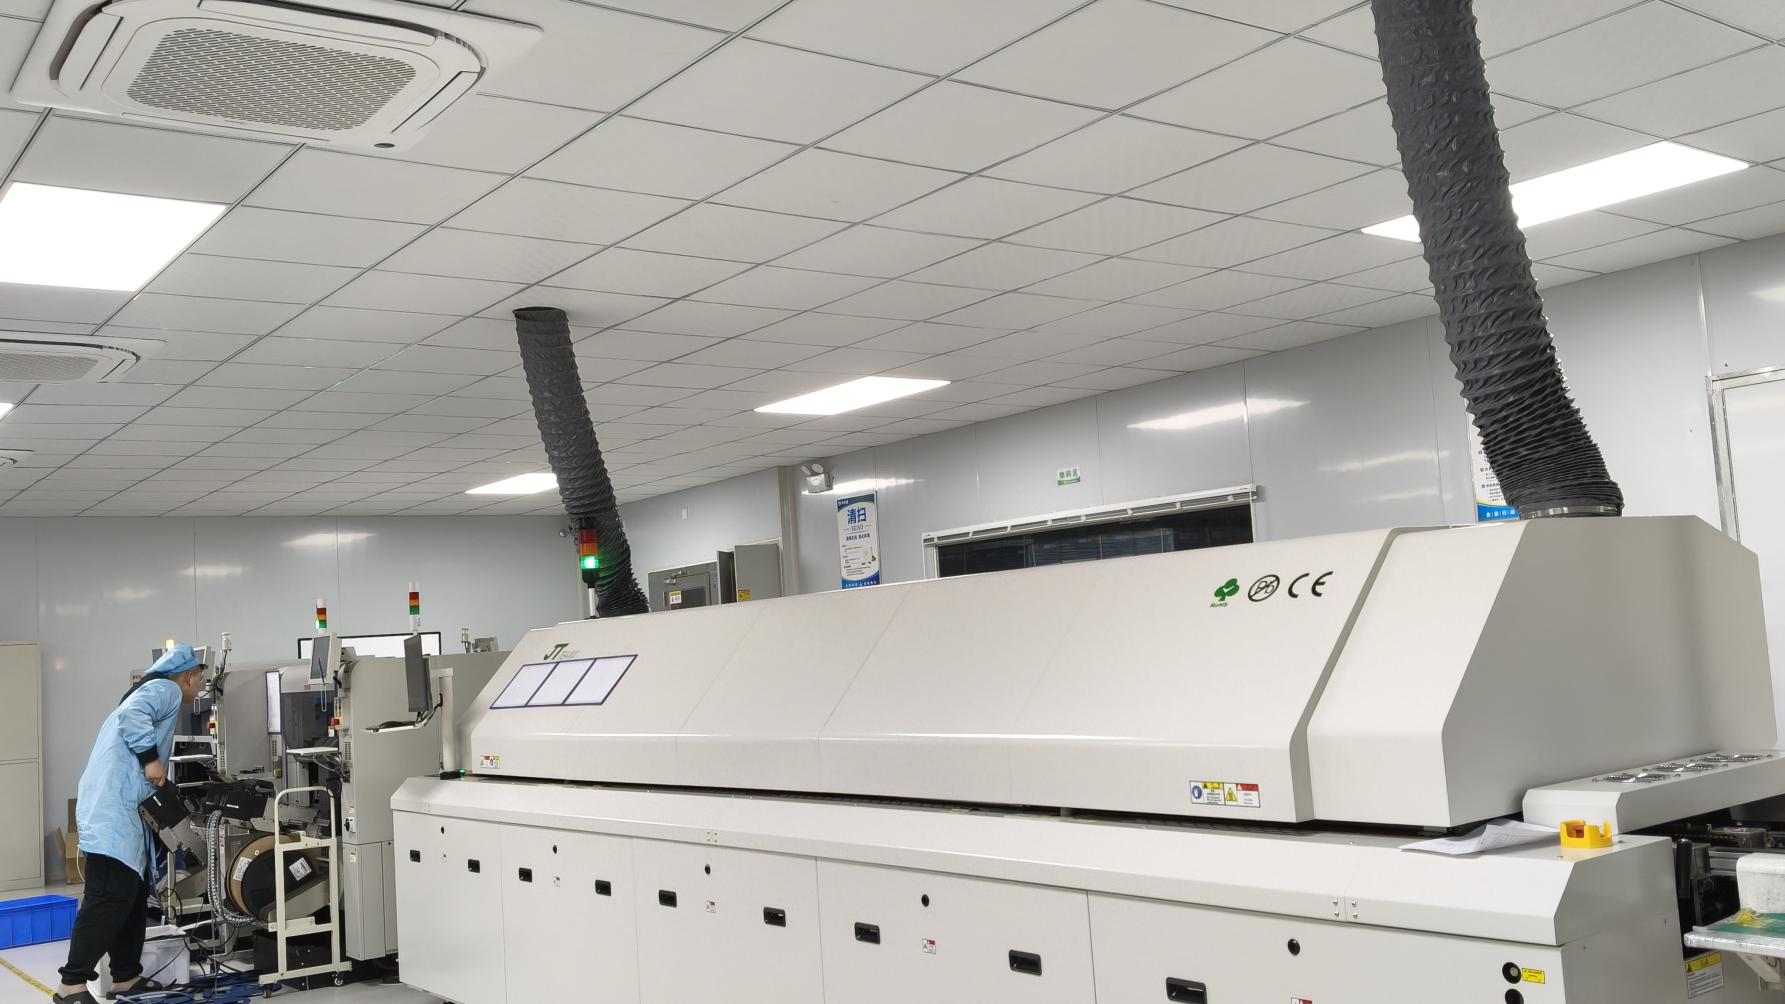
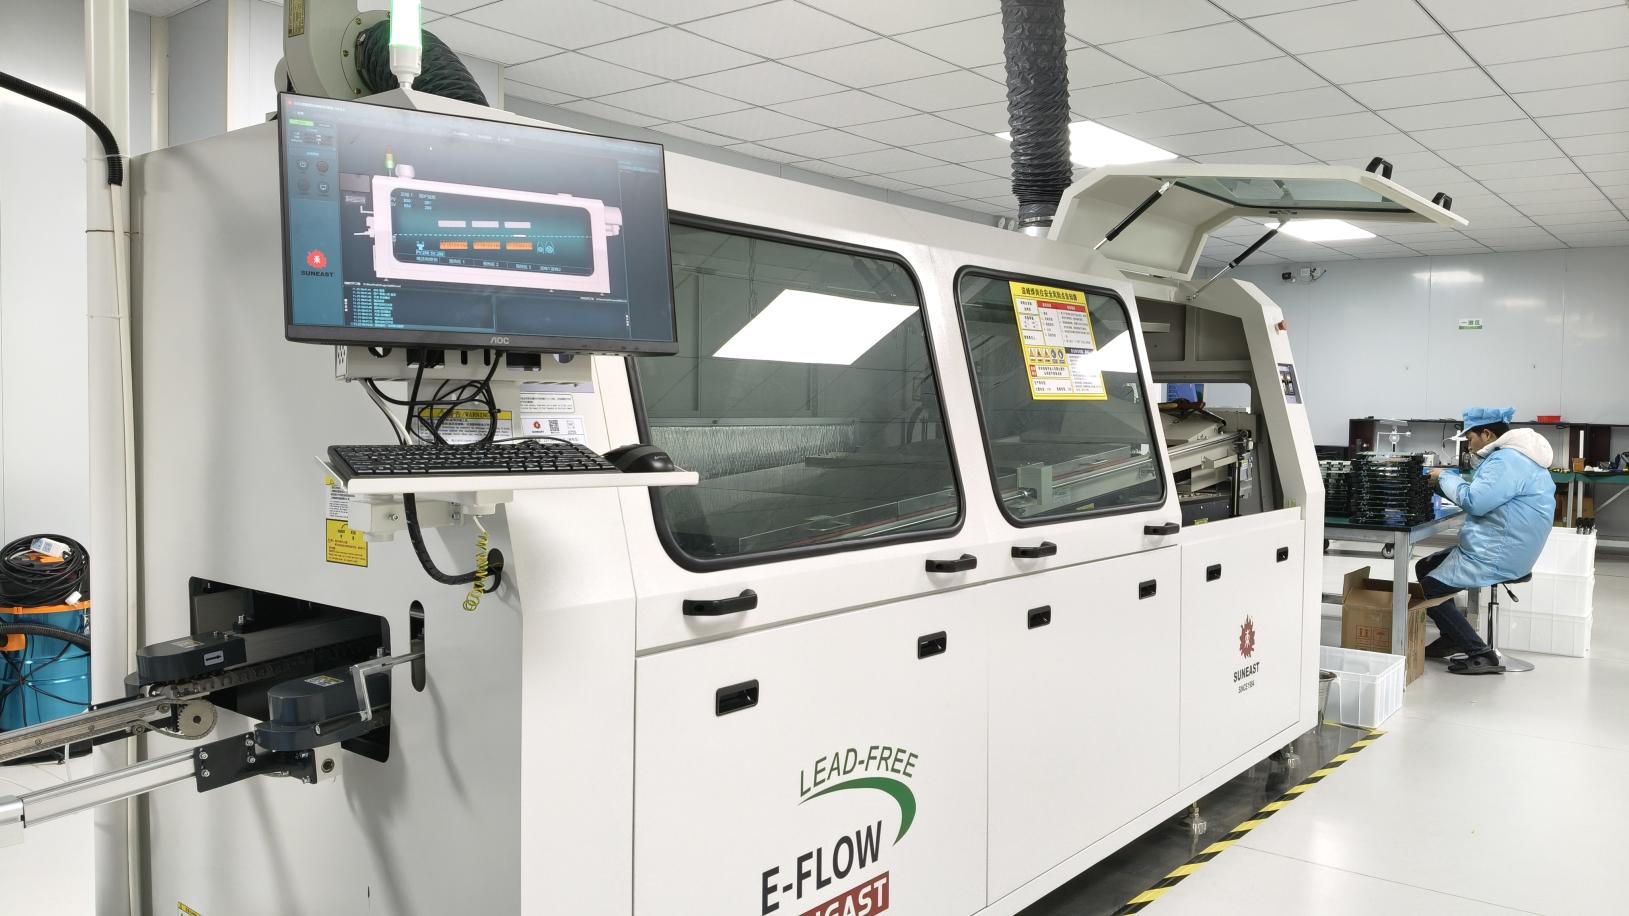
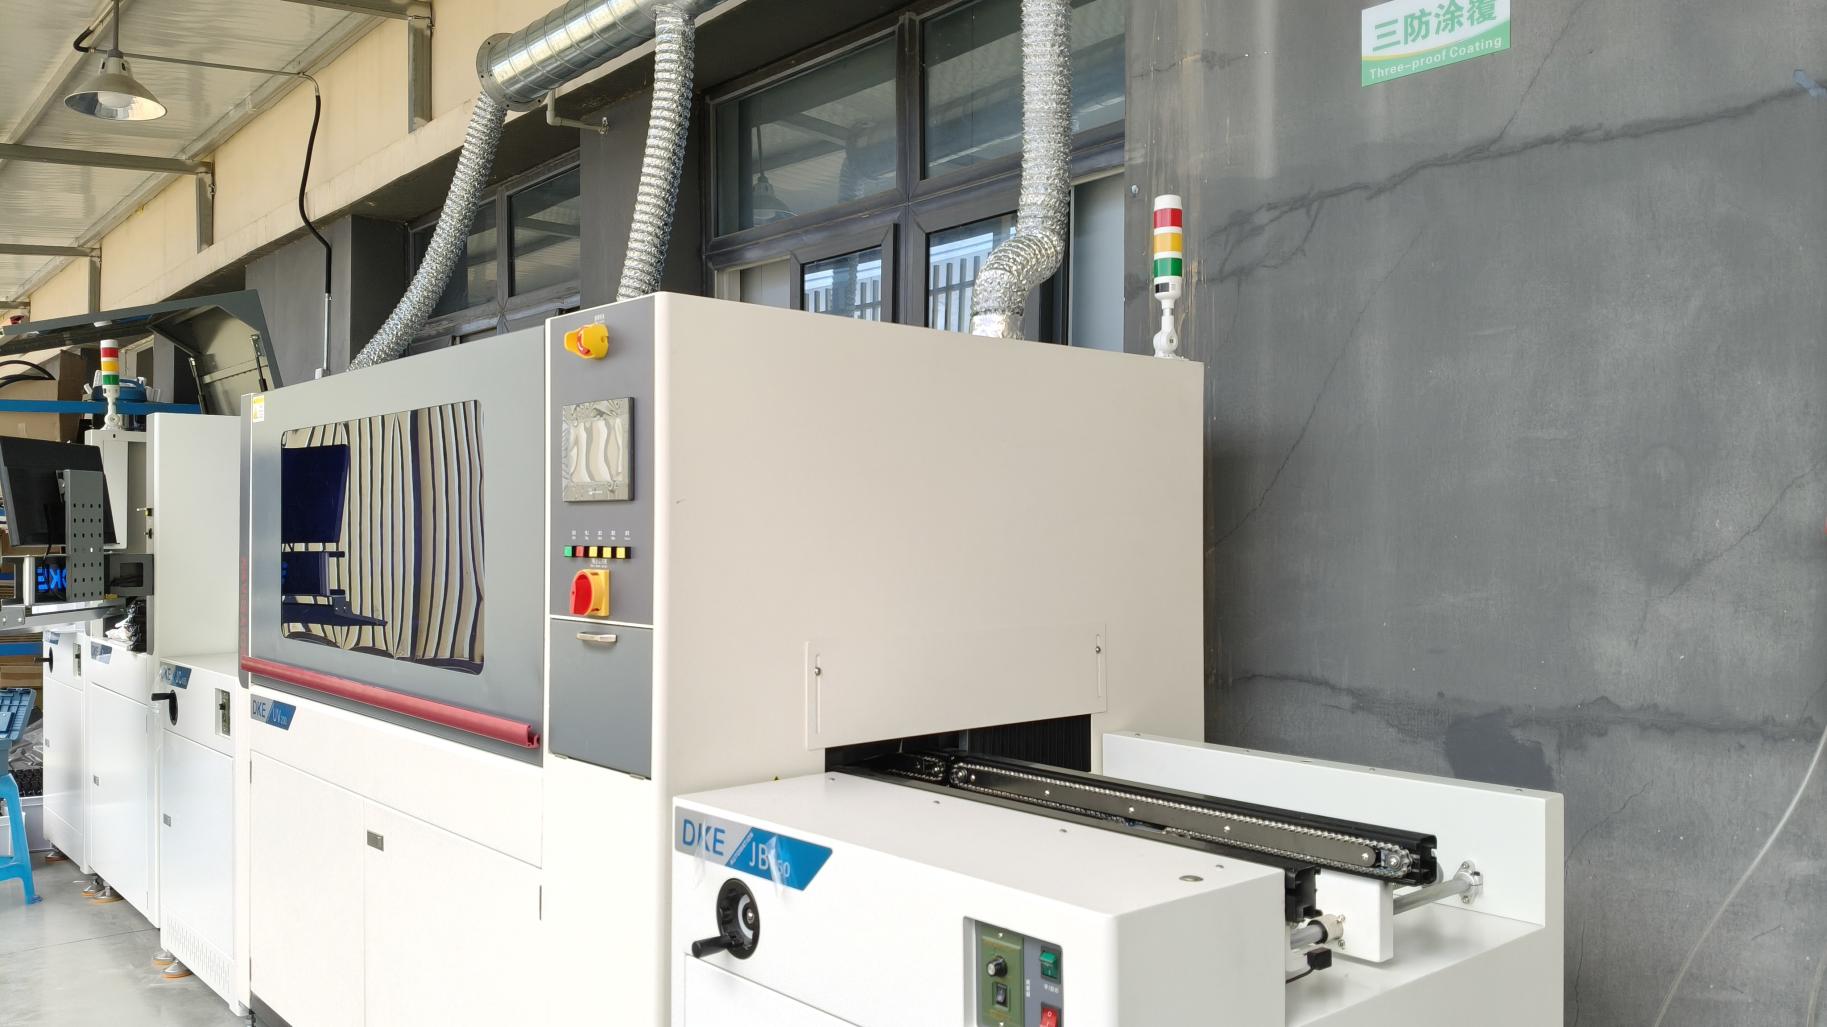
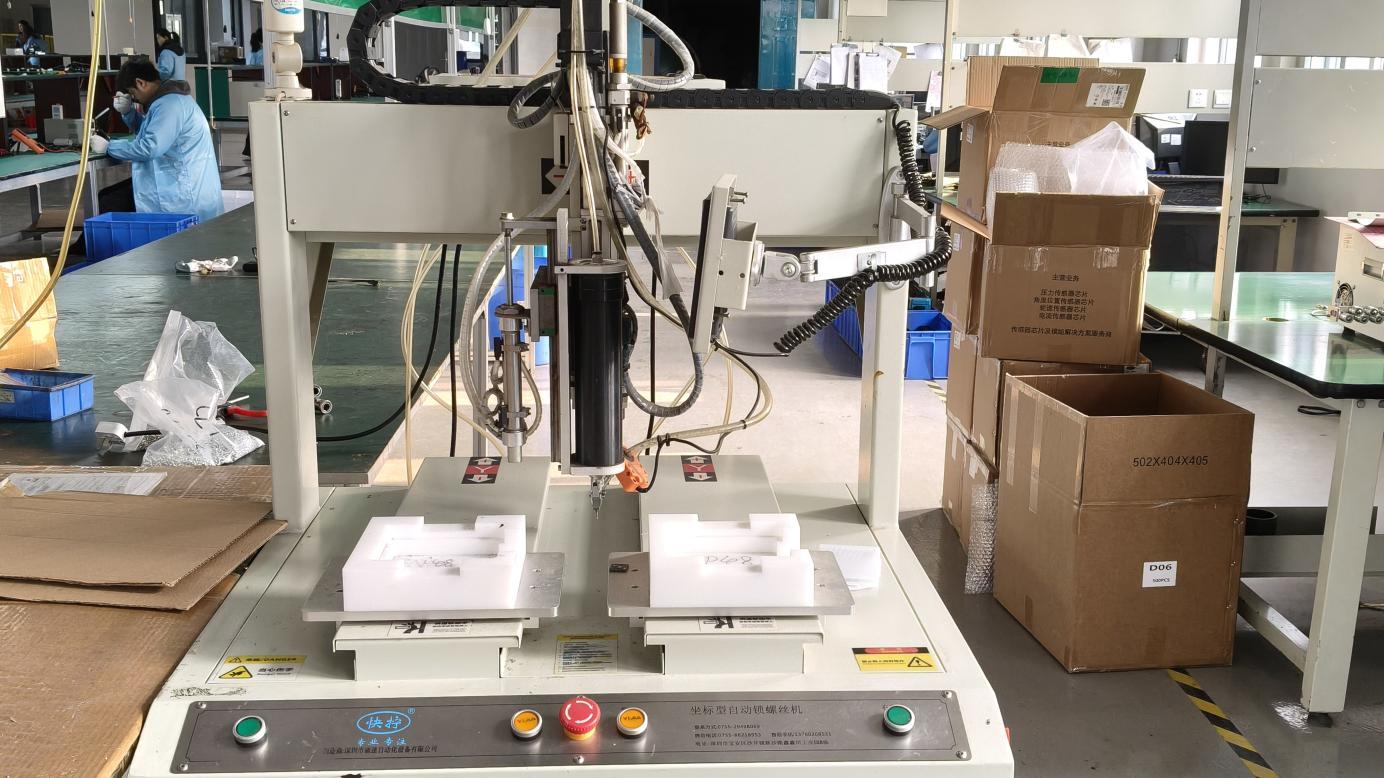
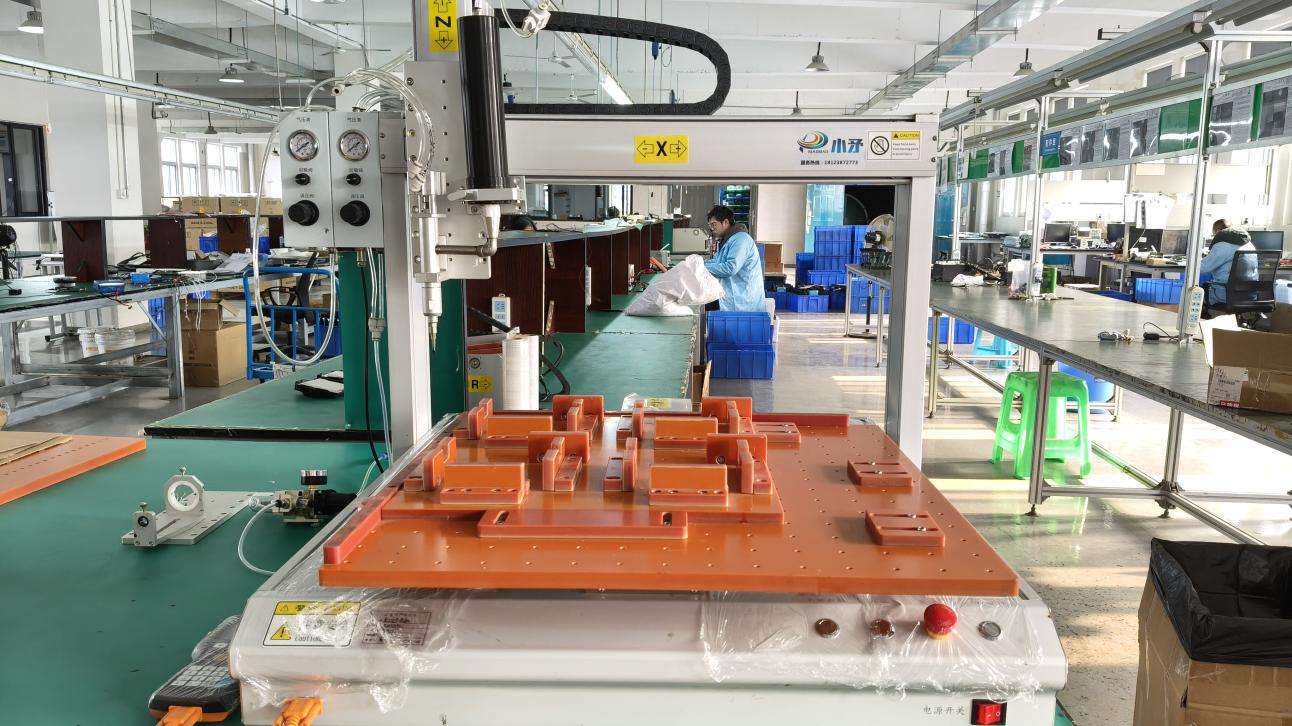
We control every step of production. Our internal workflow ensures high structural strength and precise electronic assemblies across all product lines.
As smart cities and industrial automation grow, future-proof facilities require lighting solutions designed to integrate with intelligent control ecosystems.
Our upcoming fixtures utilize Zigbee, Casambi, and DALI-2 protocols, enabling facility operators to monitor fixture health, schedule dynamic dimming, and track operational metrics remotely.
Using advanced optical silicon lenses with variable refractive indices to alter beam profiles on demand, helping warehouses adjust their floor layouts without replacing overhead lights.
Combining lithium iron phosphate (LiFePO4) battery arrays with split solar configurations allows high bay and outdoor tunnel systems to run autonomously off-grid, ensuring uninterrupted safety.
Exporting to Europe, Southeast Asia, the Americas, and Africa requires strict compliance with international standards. Our engineering workflow ensures that every high bay, solar luminaire, and floodlight meets rigorous certification benchmarks before shipment.
CE, RoHS, UL, CCC and CQC certifications ensure compliance with regional electrical safety directives.
ISO14001 certification confirms that our production processes minimize impact on the environment.
Verified IP65, IP66, and IP67 test reports ensure dependable performance in high humidity, coastal salinity, and dust.
Heavy aluminum chassis built to resist structural vibrations, dynamic wind loads, and accidental impact shocks.
Our engineering support team answers common questions from procurement specialists and lighting engineers.
Our premium LED fixtures feature an L70 lifetime rating of over 60,000 hours. We test them using continuous high-voltage aging cycles and strict junction temperature monitoring to simulate years of real-world operation.
Wattage-selectable and color temperature (CCT) tunable fixtures allow installers to customize settings on-site. This flexibility reduces the need to stock multiple fixed configurations and helps adapt to layout changes.
Our quality control process includes automated wave soldering, three-proof coating application to protect circuit components from moisture, automatic gluing for secure IP sealing, and rigorous testing in salt spray and thermal chambers.
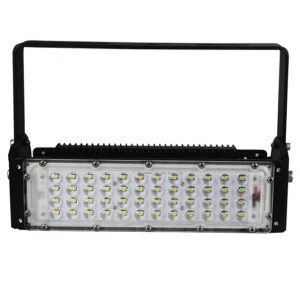
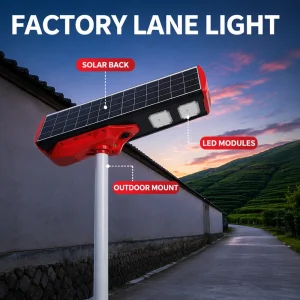
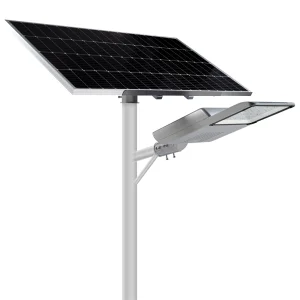
Explore our high-performance street, tunnel, and perimeter security lighting, built to handle tough outdoor environments.

 OneAll Lights